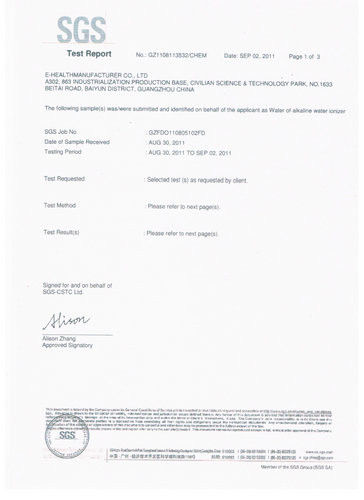
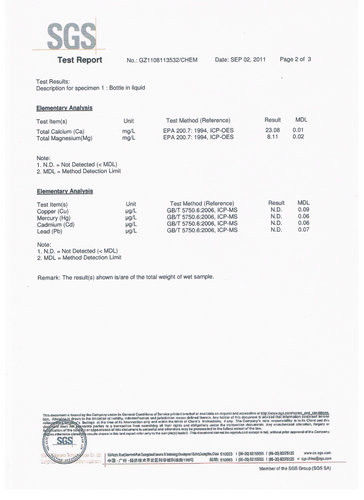
In an era demanding both operational efficiency and environmental responsibility, industries face a persistent dilemma: how to achieve thorough disinfection without chemical residues or ecological harm. A technological breakthrough now offers what once seemed impossible—water that transforms into a powerful sanitizer through electrolysis, then safely reverts to its original state.
Chapter 1: The Industrial Guardian
Food processing, agriculture, and livestock sectors have long struggled with the trade-offs of chemical disinfectants—effective sanitation versus toxic residues and regulatory burdens. Traditional methods often solve one problem while creating others.
The EHM industrial-grade electrolyzed water system presents a paradigm shift. Designed as a precision electrochemical reactor rather than a conventional water treatment unit, it delivers up to 2,000 liters per hour of both alkaline and acidic electrolyzed water. This continuous output capacity meets the demands of large-scale production while eliminating chemical dependencies.
Chapter 2: Engineering Excellence
At the system's core lies an advanced electrolytic cell engineered for industrial durability. With a lifespan exceeding 2,500 operational hours, the technology ensures stable performance in demanding environments, reducing maintenance needs and total cost of ownership.
Integrated sensors monitor oxidation-reduction potential (ORP), pH levels, and conductivity in real-time, maintaining precise water chemistry control. The 350-kilogram unit's substantial construction reflects its industrial-grade reliability, with every component designed for continuous operation.
Chapter 3: The Science of Sterilization
The system's antimicrobial efficacy stems from rigorous physicochemical principles. The produced acidic electrolyzed water achieves a pH below 2.3 and ORP exceeding +1100mV, creating an environment that disrupts microbial cell membranes and inhibits metabolic enzymes—effectively neutralizing pathogens at the molecular level.
Supplemented by 50-80mg/L of active chlorine components, the solution demonstrates broad-spectrum efficacy against bacteria, viruses, and fungi. This eliminates the need for chemical disinfectants while providing superior microbial control.
Chapter 4: Cross-Industry Applications
The technology's versatility enables transformative applications across multiple sectors:
-
Food Processing: Alkaline ion water preserves nutritional content while removing pesticide residues, extending shelf life through molecular-level preservation.
-
Agriculture: Improves livestock health and productivity while reducing antibiotic use. For crops, it serves as an organic pesticide alternative and soil remediation tool.
-
Health Management: Alkaline ion water's enhanced absorption properties support human hydration and acid-base balance.
Chapter 5: Environmental Stewardship
The system aligns with ESG principles through its closed-loop chemistry. Electrolyzed water naturally reverts to ordinary water after use, leaving no persistent contaminants. Properly stored in opaque containers below 40°C, the solution maintains its active properties for up to 90 days.
Chapter 6: Operational Parameters
Optimal performance requires input water hardness below 100mg/L, with operating pressures maintained between 0.1-0.25MPa. The system functions reliably within 5-40°C environments at humidity levels under 80%.
This electrochemical innovation represents more than advanced equipment—it embodies a fundamental rethinking of industrial sanitation that harmonizes productivity with planetary health. As industries worldwide seek sustainable solutions, electrolyzed water technology emerges as a transformative tool for the 21st century.

 ¡Su mensaje debe tener entre 20 y 3.000 caracteres!